Reduced Downtime
We work with the crankshaft in place, reducing disassembly and getting the equipment back into service faster.
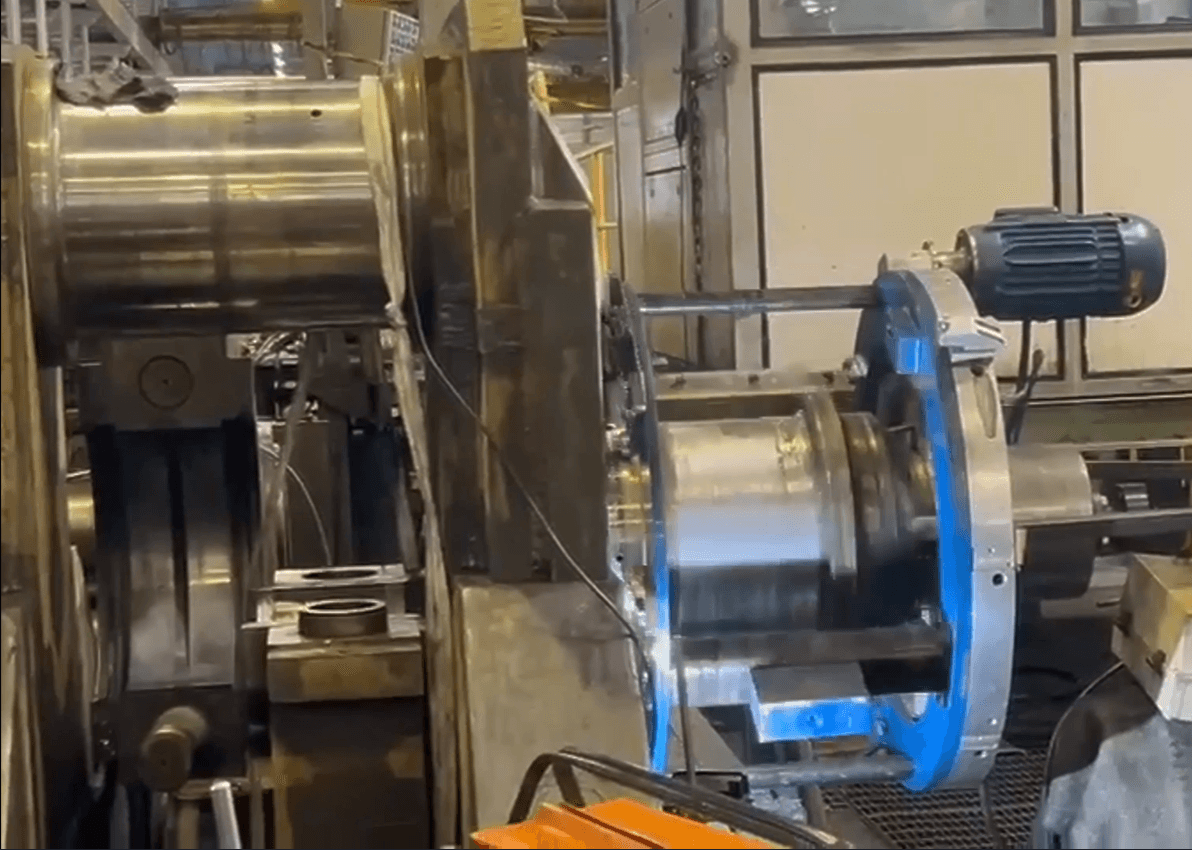
On-site crankshaft machining to correct crankpins, main journals, ovality, taper and scoring. Specialized service for industrial engines and large equipment.
Certified companyQMS CertificationWe machine crankshafts for industrial and marine engines, heavy equipment and large machinery, restoring component dimensions, alignment and operating condition.
We work with the crankshaft in place, reducing disassembly and getting the equipment back into service faster.
We remove only the material needed to correct the damage, staying within the crankshaft's dimensional limits.
We control diameter, ovality, taper and surface finish to ensure correct seating of the bearing shells.
On-site work reduces the costs and risks of removing, handling and transporting large crankshafts.
We use high-precision equipment to ensure an accurate and efficient machining process.
Correction of connecting rod crankpins affected by scoring, wear, ovality and damage caused by bearing shell failures.
Grinding of main bearing journals to restore roundness, alignment and proper lubrication conditions.
Polishing of crankpins and main journals to remove surface marks and achieve the finish specified for the bearing shells.
Correction of thrust faces affected by wear and scoring that cause excessive axial play (end float) in the assembly.
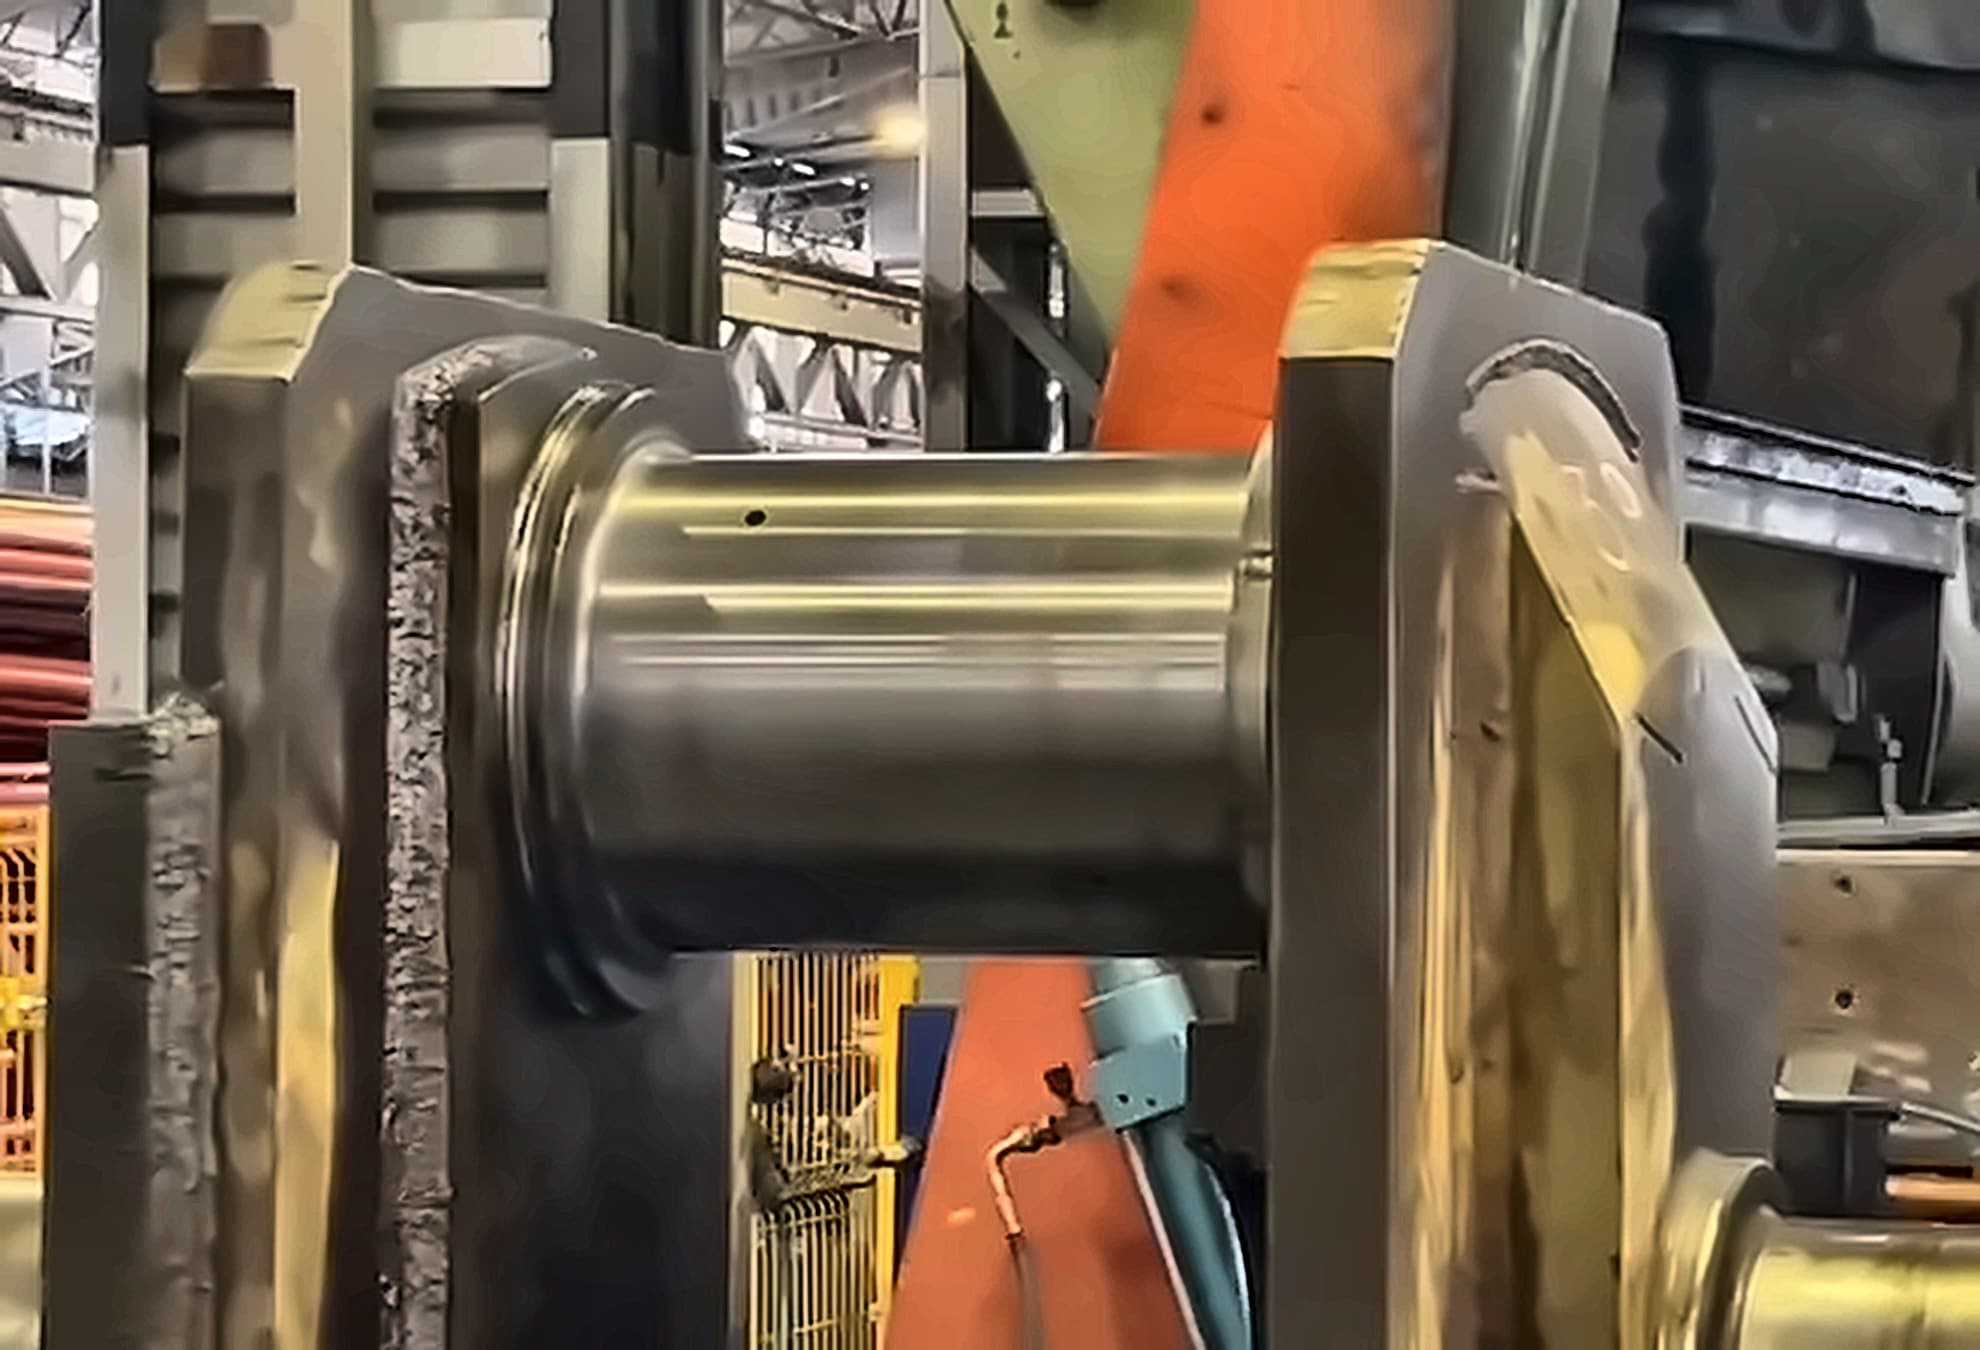
Crankshaft journal with final finish after on-site machining
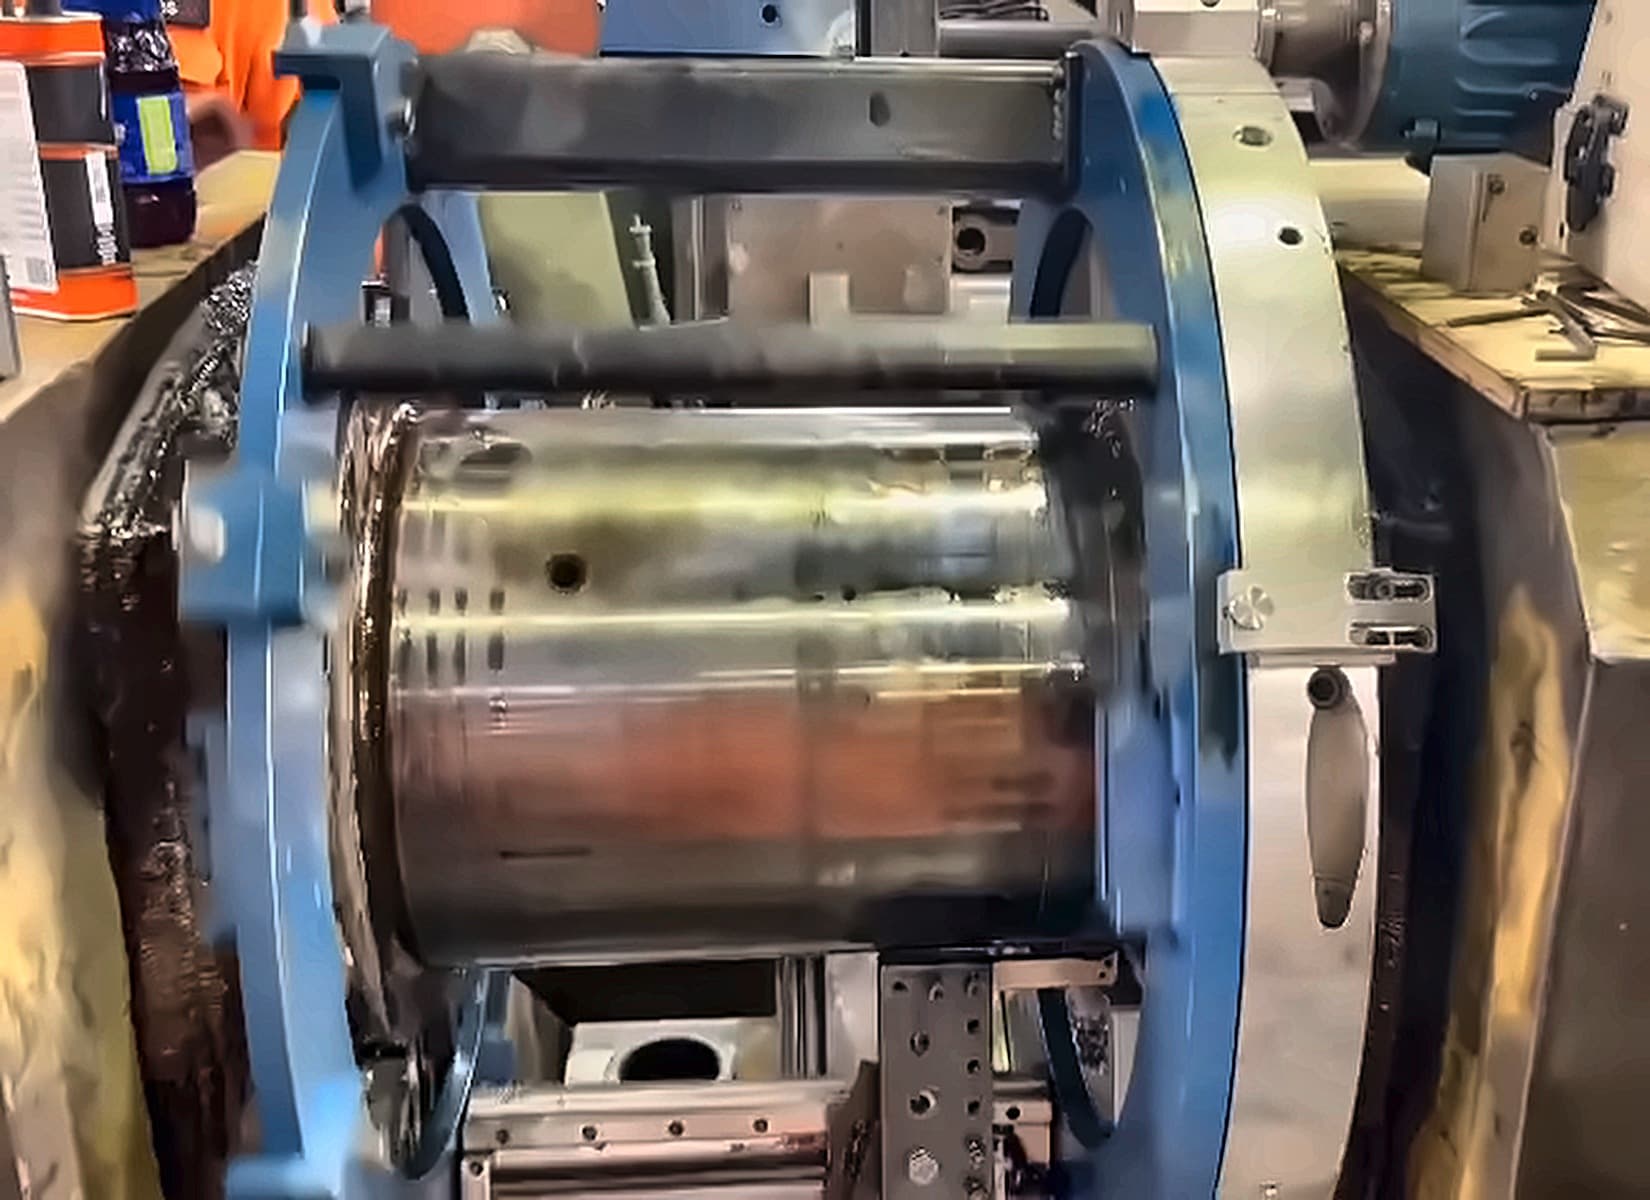
Split-type portable lathe mounted directly on the journal
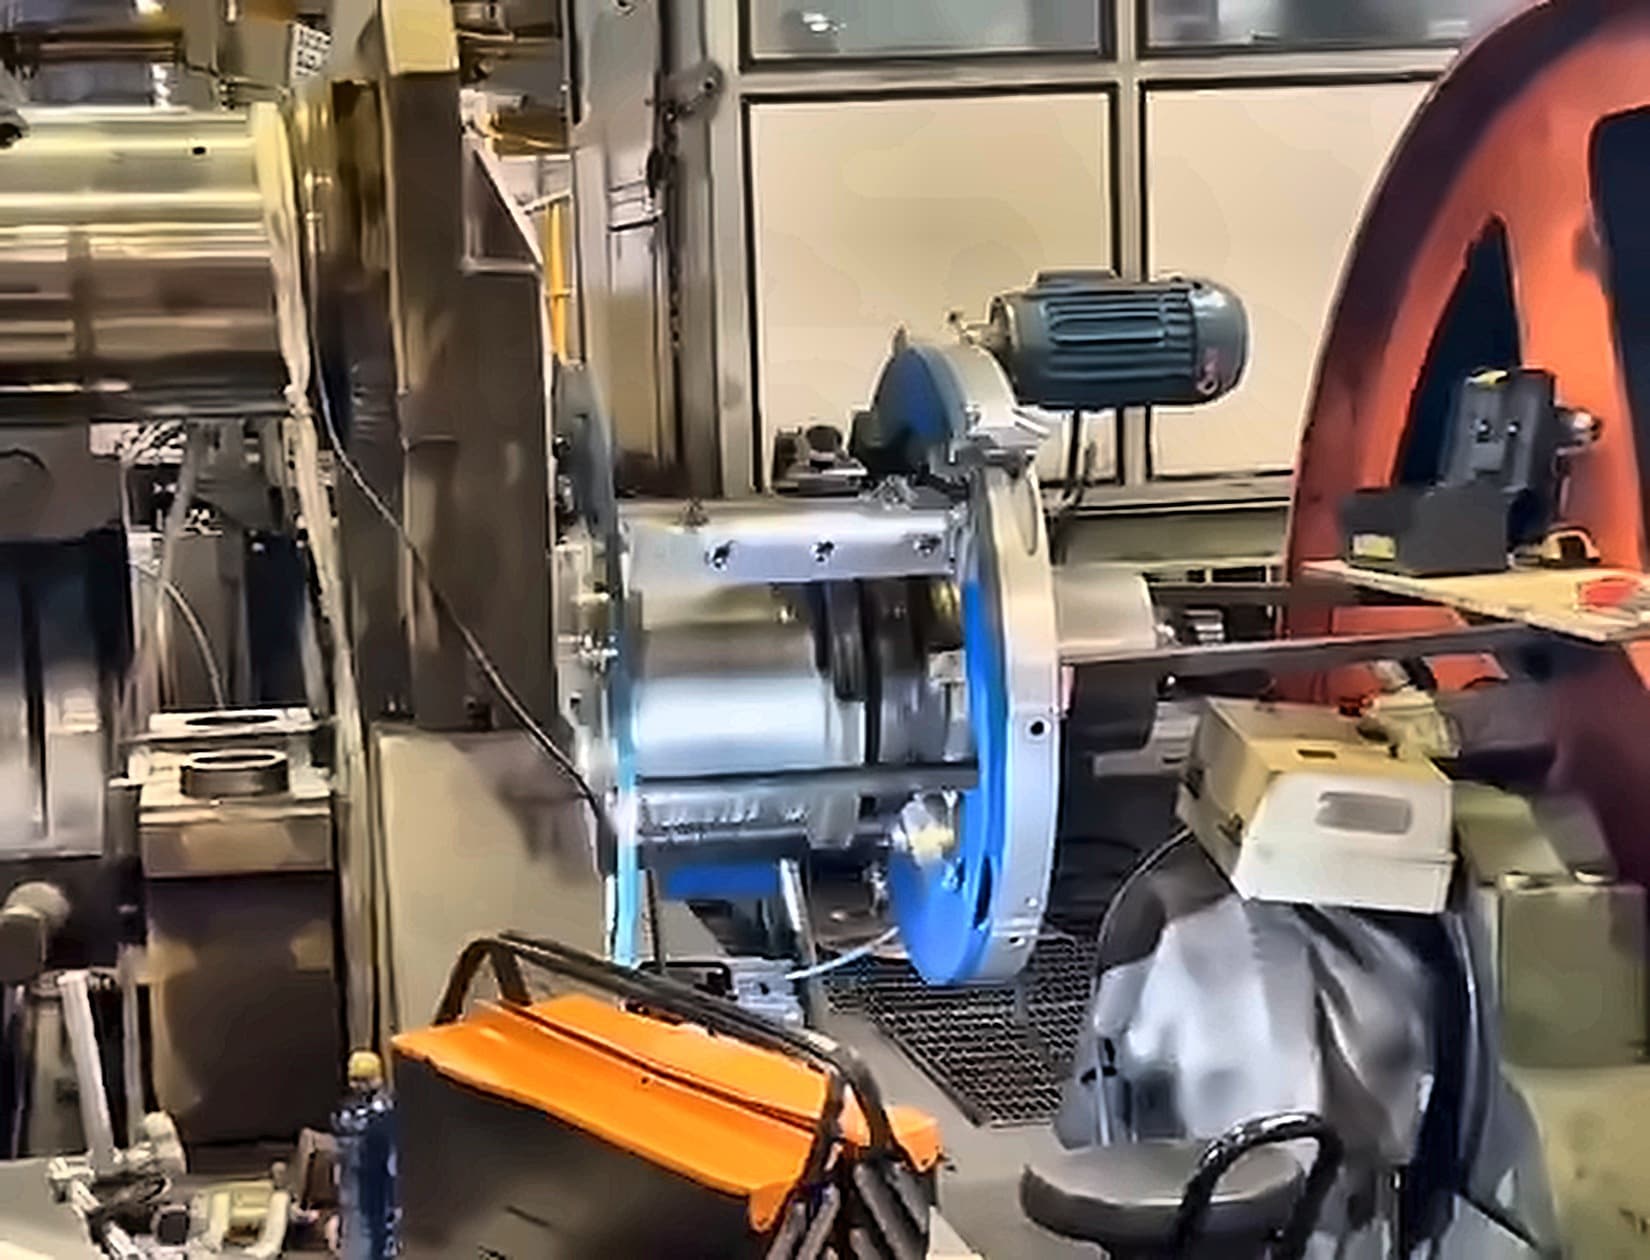
Motorized equipment machining the journal without removing the crankshaft from the machine
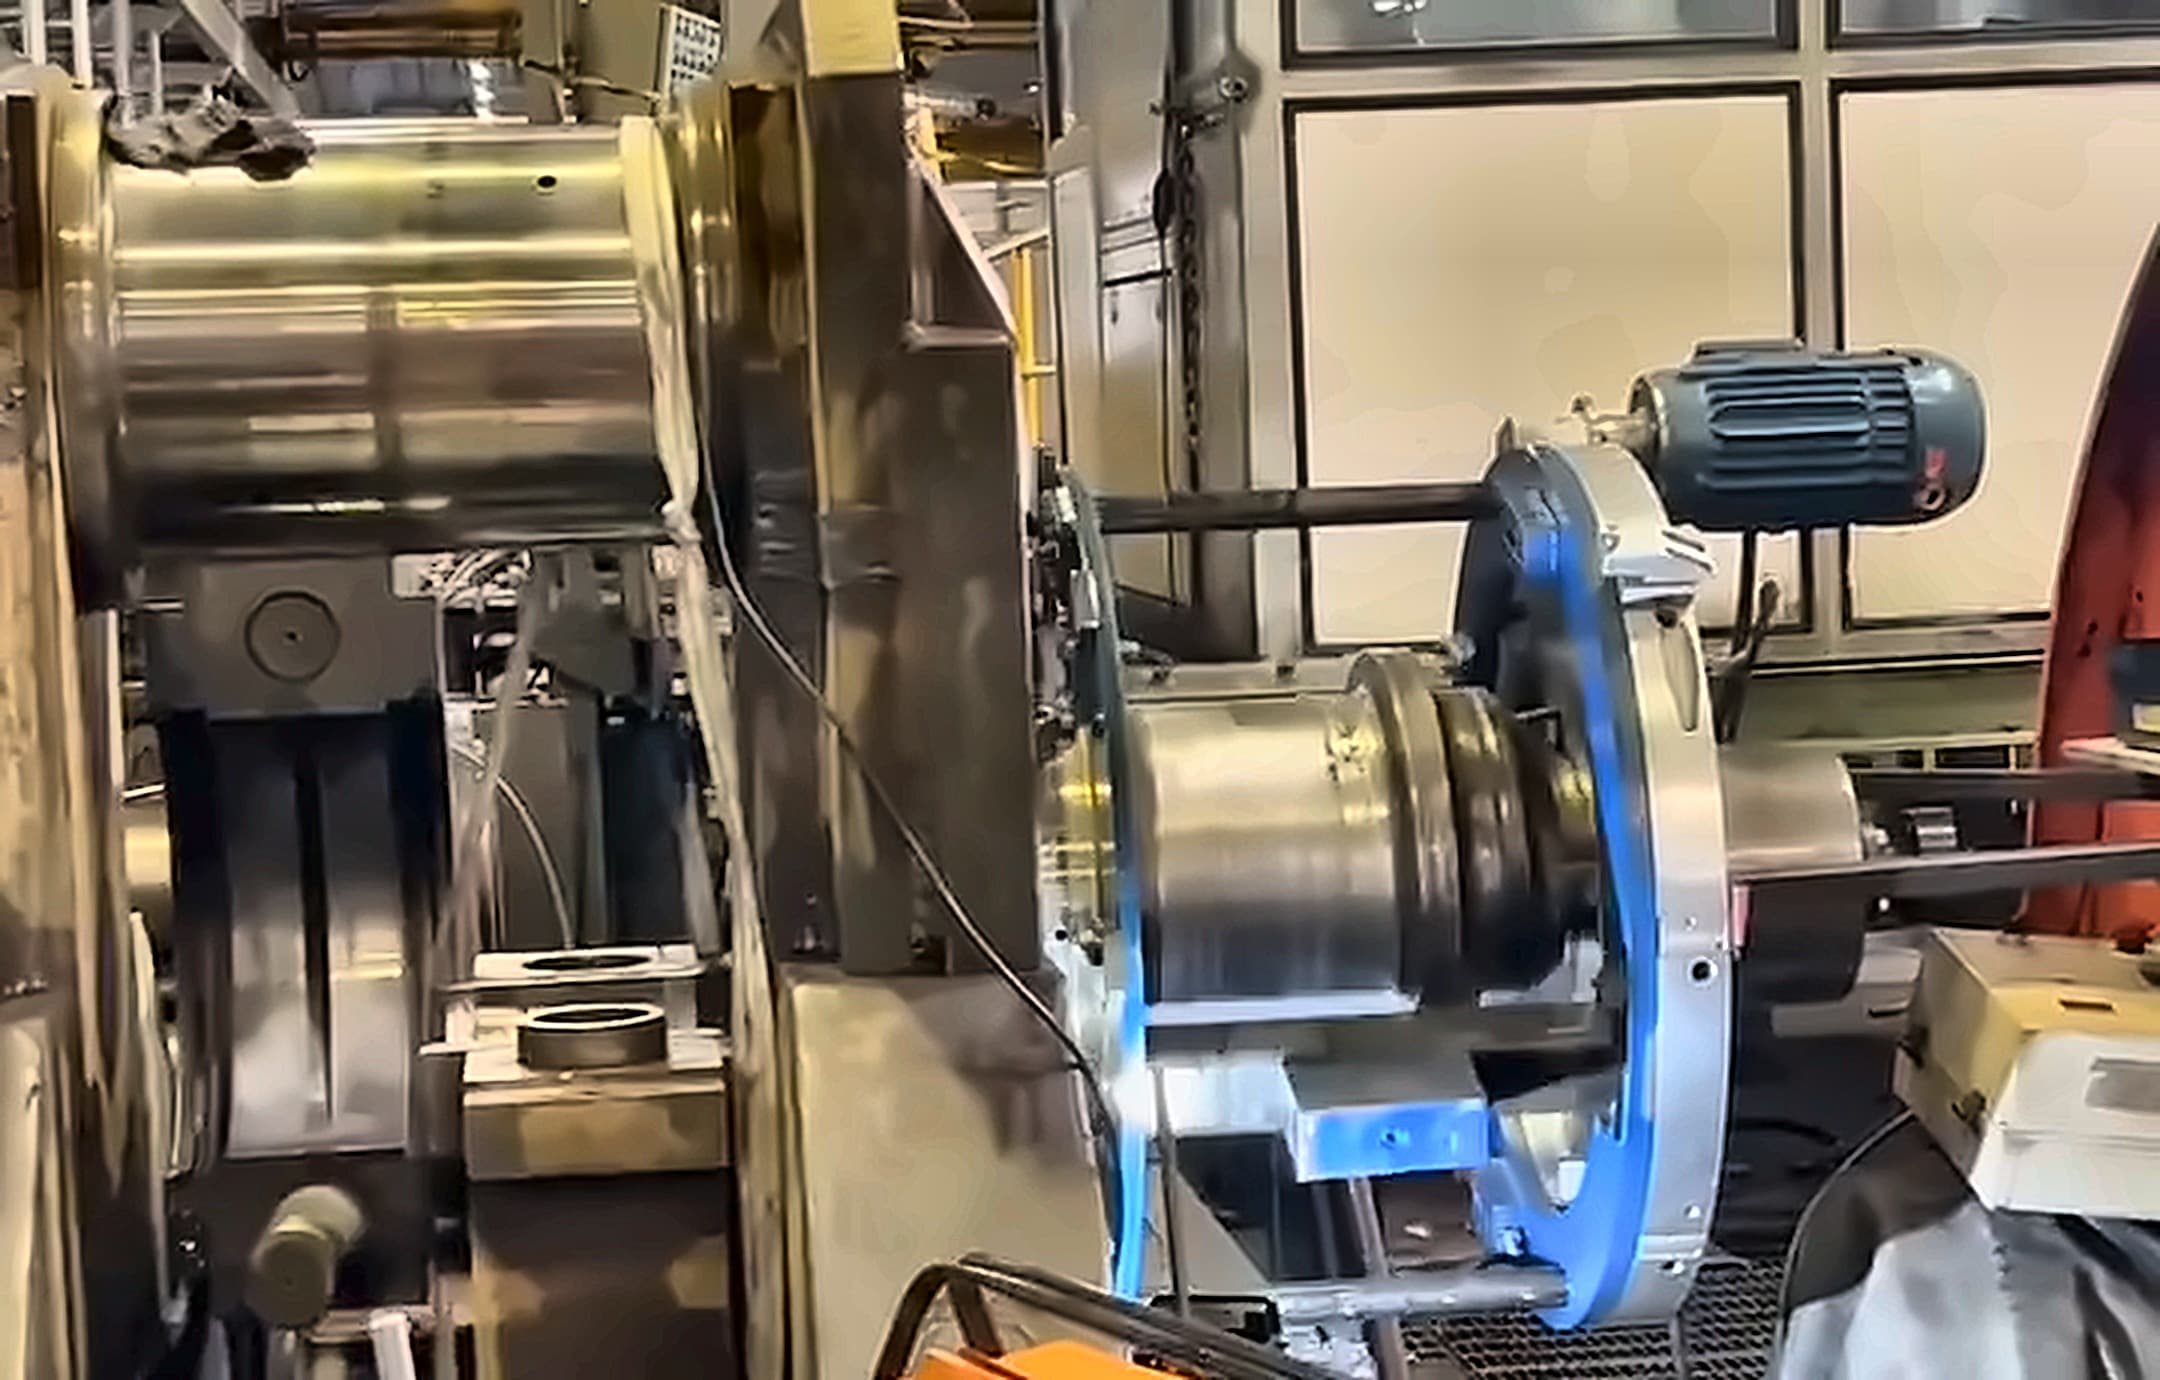
Restored journal next to the equipment set up on the next one
Join hundreds of companies that have cut costs and increased productivity with our specialized solutions